
Chapter 4
Corrosion Testing Methods and Test Planning
Written and reviewed by: Michel Comtois, M. Sc. (Physical Chemistry) and Anne-Marie Comtois, Eng. — August 1, 2026
Corrosion testing exposes materials, coatings, or finished products to controlled corrosive conditions so their performance can be evaluated. The appropriate method depends on the material, expected service environment, likely corrosion mechanism, and purpose of the test. Common approaches include salt spray, cyclic corrosion, humidity, immersion, atmospheric exposure, and combined corrosion-weathering testing.
How is Corrosion Testing Done?
There are many types of tests for corrosion, depending on the variables and environment your material will be subjected to in real life, including:
- Electrochemical
- Cabinet (salt spray fog, humidity, corrosive gas, cyclic)
- Immersion
- High-temperature and high-pressure
- Atmospheric
- Seawater
- Freshwater
- Soils
- Industrial application
THE MOST WIDELY USED METHOD
Salt Spray Testing: From Basic to Cyclic
A popular standardized test method for corrosion testing is “salt spray testing,” as it provides good repeatability without being too expensive. It is used to assess the corrosion resistance of coated or otherwise surface-treated samples.
Many test methods can be carried out using salt spray, as seen in our Table of Standards, which describes multiple corrosion testing methods in detail. Although many industries prefer to do corrosion tests using traditional steady-state methods, cyclic corrosion testing is more representative of the product’s environment.
The first recognized accelerated corrosion test can be traced to 1914, when the Sherwin-Williams Company in Cleveland developed the “salt spray test.” It then evolved to become the first accelerated corrosion practice and was published by ASTM in 1939 as ASTM B117. Since then, it has been revised on many occasions.
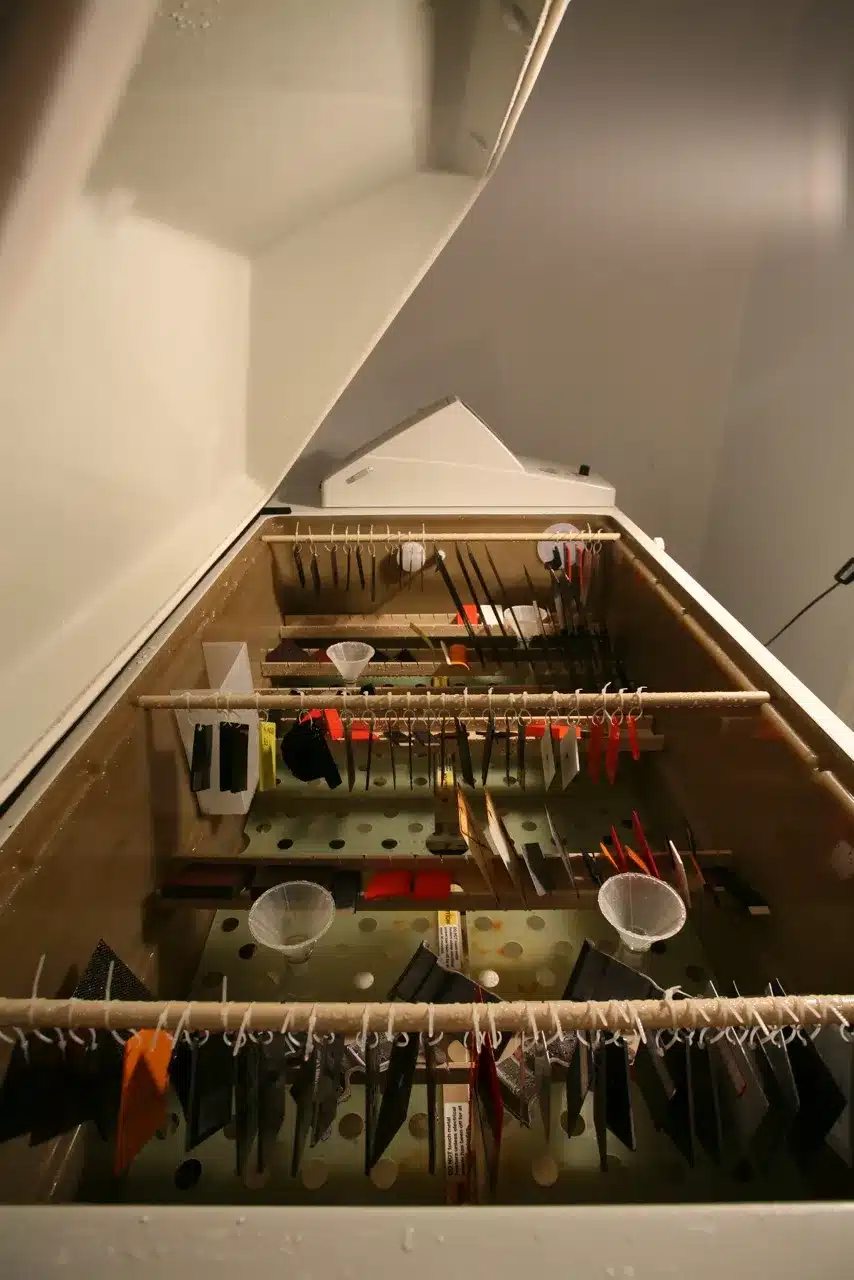
Salt spray testing per ASTM B117 is arguably the best known and still the most widely used corrosion practice in the world. Numerous test methods (MIL-STD, SAE, and even other ASTM methods) still refer to ASTM B117 for corrosion testing, even if more specific and more advanced test methods are now available. The main reason remains that so many companies worldwide have extensive data on the behavior of their products and materials under ASTM B117 conditions, which makes them reluctant to adopt newer methods and risk decades of collected information becoming useless or, at least, less relevant.
Although ASTM B117 is not a good simulation of outdoor exposure as it has a poor rank order correlation, it does have good repeatability and reproducibility, which are key advantages. The testing is also easy to perform, thus being less costly. It is mainly used for quality control or as a comparative tool. This test uses a fine mist of 5% NaCl at 35°C and neutral pH. As a classic corrosion testing method, the conditions are steady-state.
As discussed in Chapter 3, there are different corrosion mechanisms, and not all of them appear under ASTM B117 conditions. ASTM B117 uses static, steady-state conditions that are rarely representative of real service environments. Cyclic tests were therefore created to better simulate specific environments.
GREATER REALISM
Toward More Sophisticated Cyclic Tests
Cyclic Corrosion Testing
The cyclic corrosion testing method is intended to be a more realistic way to perform salt spray tests than traditional steady-state exposure tests. Since actual atmospheric exposures usually include both wet and dry conditions, cyclic corrosion testing can pattern accelerated laboratory tests after these natural cyclic conditions.
Research indicates that cyclic corrosion testing produces relative corrosion rates, structure, and morphology that are more similar to those observed outdoors. Consequently, this approach usually provides a better correlation to outdoor environmental conditions than conventional salt spray tests.
Cyclic corrosion tests are effective for evaluating a variety of corrosion mechanisms, including general, galvanic, and crevice corrosion. Simple exposures, such as prohesion, may involve cycling between salt fog and dry conditions. More sophisticated automotive methods call for multi-step cycles that incorporate immersion, humidity, condensation, along with salt fog and dry-off. There are many ways to test for corrosion resistance using cyclic corrosion, including the ASTM G85, ASTM G44, and ASTM D5894 tests.
ASTM G85
ASTM G85 can be seen as an improved version of ASTM B117 to some extent. The standard uses the basic principles of ASTM B117 but adds specific requirements for certain industry sectors to address their particularities. The use of a different salt combination (to emulate seawater, for example) or a different pH is a typical example. A choice of different cycles (test conditions) within the ASTM G85 standard must be made, depending on the real-life environment surrounding the item. These cycles are presented in more detail in the following Table of Standards.
ASTM D5894
ASTM D5894 integrates more natural factors than traditional corrosion tests like ASTM B117 or ASTM G85. By integrating the effects of UV, temperature, and humidity variations, ASTM D5894 improves the correlation with natural corrosion observed in the field. ASTM D5894 offers a “standard” recipe (ASTM G154 cycle 2 / ASTM G85 annex 5), and an increasing number of manufacturers are adopting those test parameters to match their realities. For example, by increasing the UV period, you can better simulate Middle Eastern conditions, or by changing the electrolyte composition, you can more realistically mimic urban environments.
SAE J2334
SAE J2334 (Society of Automotive Engineers) is a corrosion cycle test using the following electrolyte solution:
- 0.5% NaCl
- 0.1% CaCl₂
- 0.075% NaHCO₃.
For each cycle, samples are conditioned at 50°C and 100 % RH for 6 hours, then sprayed or immersed in the solution specified above for 15 minutes, and finally dried at 60°C and 50 % RH for 17.75 hours. The test is done for a given number of cycles, depending on the test requirement.
ASTM B117 vs. ASTM G85 vs. ASTM D5894
Neutral Salt Spray — ASTM B117
Advantages: Good repeatability and reproducibility. Easy to perform and operate. Lots of data. Low cost.
Disadvantages: Not a good simulation of outdoor exposure (poor rank correlation).
Cyclic Corrosion — ASTM G85
Advantages: Specificities of industries (salt combinations). Choice of different cycles. Good simulation of outdoor environments.
Disadvantages: More costly and less data available for comparison purposes.
Cyclic Corrosion — ASTM D5894
Advantages: Integration of natural factors (UV, temperature, humidity). Great simulation of outdoor environment.
Disadvantages: More costly and less data available for comparison purposes.
Combined Testing
The table below illustrates the correlation between a laboratory testing method and a severe corrosion environment. Although ASTM B117 is by far the most popular method, it is mostly used as a comparative or pass/fail tool. To get a better correlation, combined testing methods were developed, which include cycles alternating salt spray testing and UV testing. The results give more representative data since, for example, when coatings degrade from UV exposure, they can become more susceptible to corrosion. Other, more sophisticated methods, such as the ASTM D5894 standard, exhibit even higher correlation rates. They include multi-step cycles that incorporate ambient, humidity, condensation, or other conditions in addition to salt spray and dry-off. As for prohesion, it may be described as simple cycles between salt fog and dry conditions.
| Laboratory test method | Correlation with severe marine environment |
|---|---|
| Conventional salt spray (ASTM B117) | −0.11 |
| Prohesion (e.g. ASTM G85) | 0.07 |
| Cyclic immersion with UV | 0.61 |
| Combined corrosion/weathering (ASTM D5894) | 0.711 |
Note: Correlation values are illustrative and may vary depending on coating system and exposure site.
DURATION
How Long Does a Corrosion Test Last?
Just like their colleagues from the weathering community, corrosion experts have tried to find, without remarkable success, that magic number. No matter how the question is formulated, the answer is always the same: “It depends!” And it depends for one simple reason: outdoor conditions cannot be controlled the way laboratory conditions are!
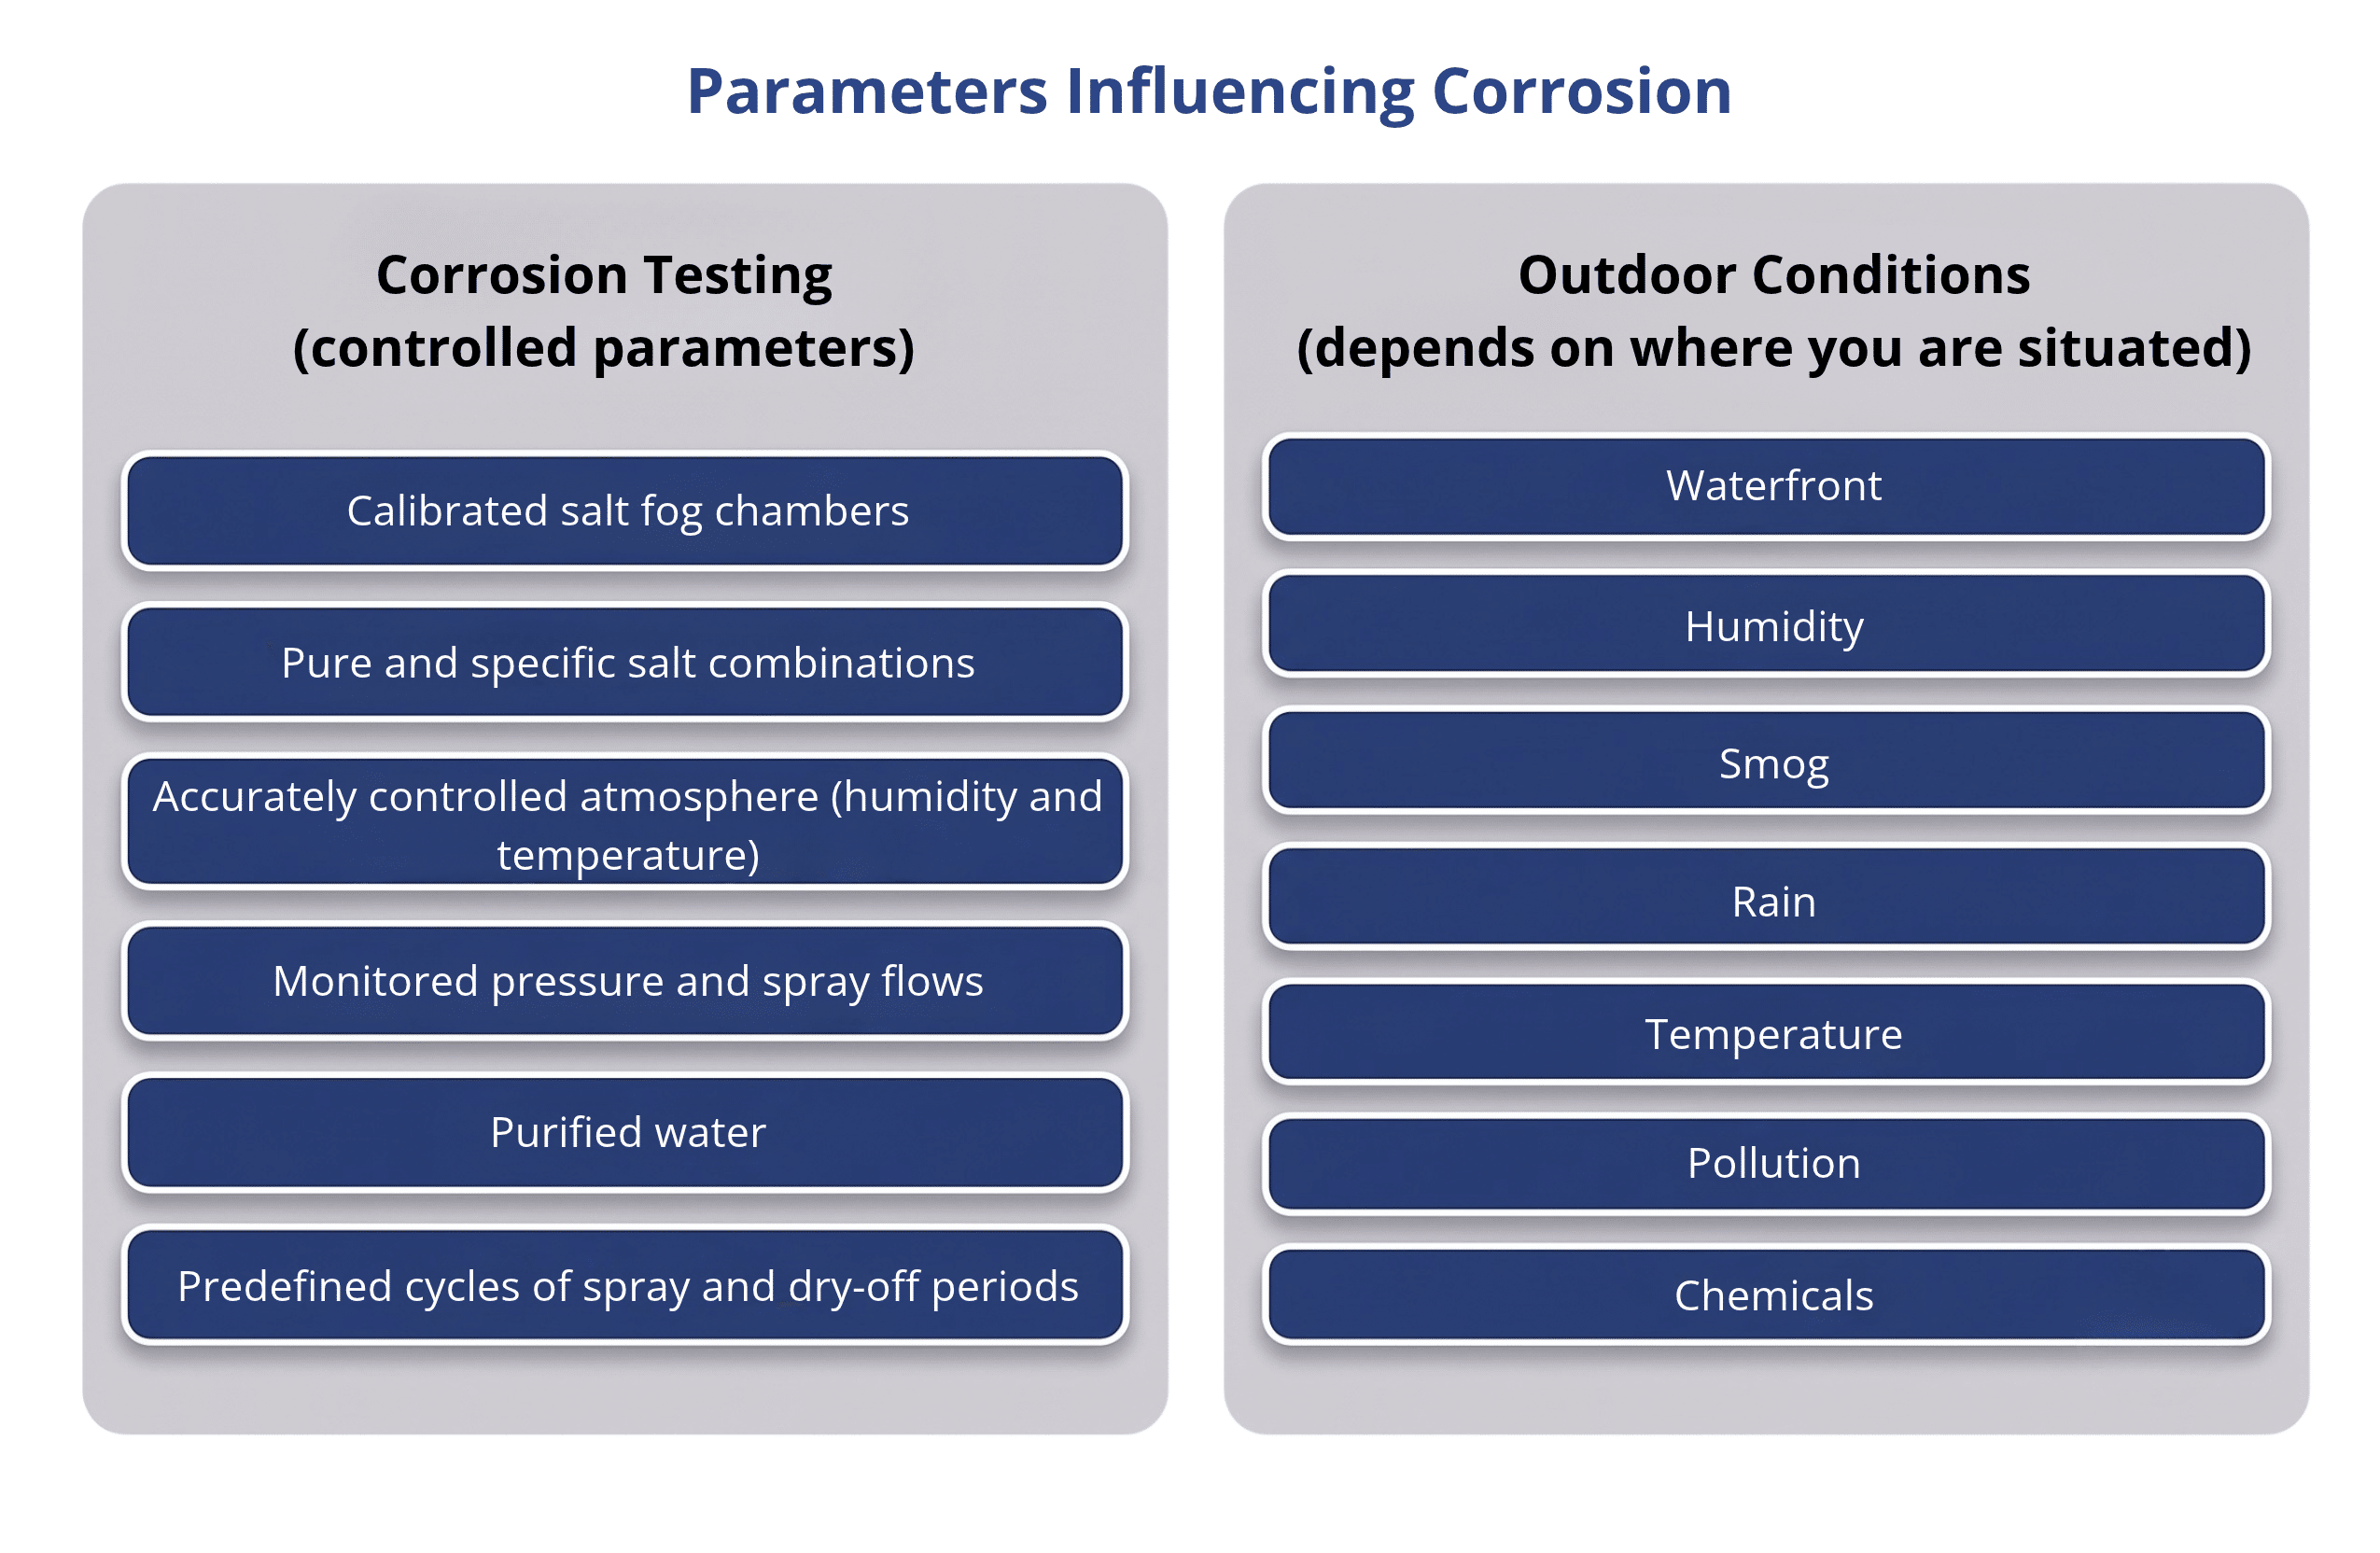
All parameters — waterfront, humidity, smog, rain, temperature, pollution, chemicals, and more — have a significant influence on the severity of outdoor corrosion.
There is no universal acceleration factor for corrosion testing. An acceleration factor should only be used when a reliable correlation between laboratory exposure and actual service exposure has been demonstrated for the specific material, coating system, corrosion mechanism, and environment being evaluated. In most cases, accelerated corrosion testing is therefore used for comparison, qualification, quality control, or failure investigation rather than as a direct predictor of service life.
For this reason, test duration should be determined based on factors such as:
- an applicable specification;
- historical performance data;
- an established correlation;
- a pass/fail objective;
- a control product;
- acceptance criteria.
A longer exposure is not automatically more representative.
The table below shows common test durations used across various industry sectors.
Examples of Exposure Durations Commonly Specified in Certain Industrial Standards
| Sectors | Test Durations | Products | Criteria |
|---|---|---|---|
| Defence | 1,000 hrs of ASTM B117 | Primers and epoxy coatings | ASTM D1654 |
| Up to 240 hrs of ASTM B117 | Electronic parts | Functional | |
| Architecture | 1,500 hrs of ASTM B117 | Organic coatings (minimum requirements) | ASTM D1654 |
| 3,000 hrs of ASTM B117 | High-performance organic coatings | ASTM D1654 | |
| 4,000 hrs of ASTM B117 | Superior performance organic coatings | ASTM D1654 | |
| Automotive | 1,500 to 4,000 hrs of ASTM B117 | Coatings, mechanical parts, and welds | Various |
| Structure | 800 hrs of ASTM B117 | Base test on coated materials | ASTM D610 ASTM D714 |
| 10,000 hrs of ASTM D5894 | Galvanized structures | Various | |
| Consumer Goods | 96 to 1,000 hrs | Bare and coated metals | ASTM D610 ASTM D714 |
Important: These durations are examples drawn from selected specifications and applications. They are not universal requirements and should not be used to predict service life. The applicable test duration must be determined from the relevant specification, customer requirement, historical correlation or defined acceptance criteria.
MEASURING OUTCOMES
Evaluations During a Corrosion Test
Measurements at various time intervals can be quite useful during the corrosion testing process for your samples. This investment may help you save money down the road if you need to end the tests sooner and avoid wasting your time. If your product does sustain the entire testing process, this type of data will be useful to identify the behaviour of your product more accurately over time. In fact, more often than not, the corrosion of a material cannot be described as linear. Having additional data in your hands may help you extrapolate more accurately the deterioration of a particular material or product within its life span.
Most Popular Evaluations
Among the tests below, ASTM D610, ASTM D714 and ASTM D1654 can be used to evaluate sample performance at various time intervals during the corrosion test, while the other test methods are usually performed once the exposure is completed, as they damage the surface.
Degree of Rusting — ASTM D610
Photographic rating scale for the percentage of rust visible on a metal surface.
Degree of Blistering — ASTM D714
Rates the size and frequency of blisters in a coating during or after corrosive exposure.
Evaluation of Coated Specimens — ASTM D1654
Rates creepage: how far corrosion has spread from a deliberate scratch (scribe) in the coating.
Tape Adhesion — ASTM D3359
Cross-cut and tape test to assess how well a coating adheres to the substrate after corrosive exposure.
Film Hardness — ASTM D3363
Pencil hardness test to measure the mechanical integrity of a coating after aging.
Pull-off Strength — ASTM D4541
Measures the tensile force required to detach a coating from a substrate. Most relevant for thick industrial coatings.
Corrosion Measurements
To determine the corrosion rate from mass loss, the following calculation may be done2. This method of measurement is referred to in the ASTM G1 standard: Practice for Preparing, Cleaning, and Evaluating Corrosion Test Specimens.
T = time of exposure (hours)
A = area (cm²)
W = mass loss (g)
D = density (g/cm³)
YOUR CHECKLIST
Preparing a Test Plan
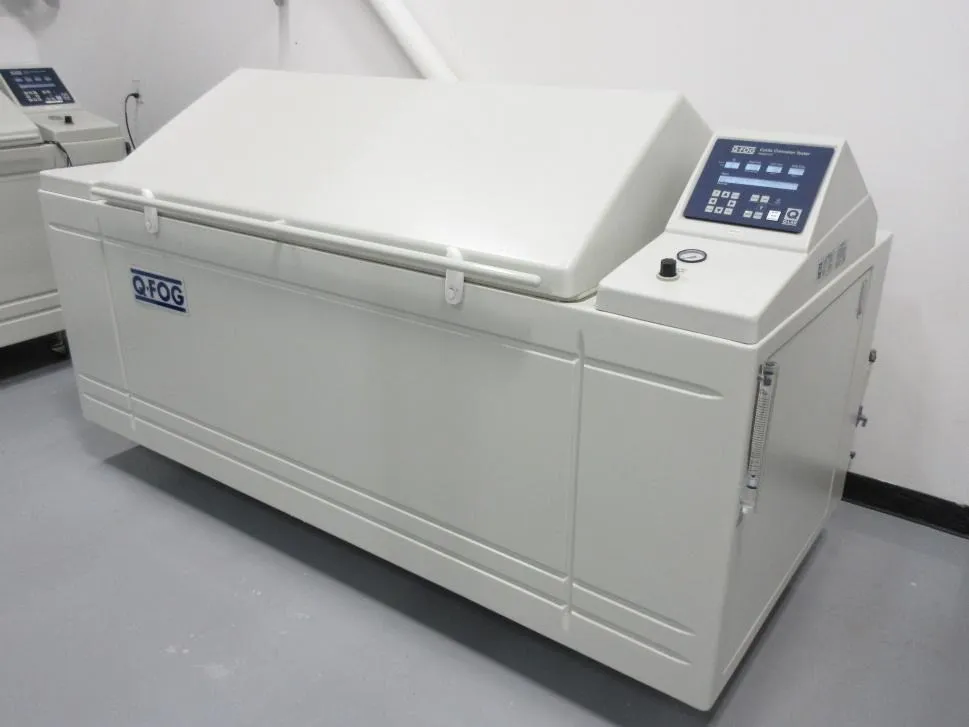
Corrosion testing is often performed in a fog spray chamber in which a specific cycle can be programmed. Specimen size and geometry depend on the applicable method, product, chamber capacity, and evaluations to be performed. Flat test panels measuring approximately 3″ × 6″ are commonly used in some corrosion-testing programs, but this is not a universal specimen size. Larger or finished components can also be accommodated depending on the test method and equipment.
To prepare a test plan that will suit your needs, the following factors should be considered:
Why do you need corrosion testing?
What type of corrosive environment will your product be subjected to? Defining the required operating conditions will make it easier to determine the appropriate standard and, if not, customize a proper test plan. If testing is done for comparison purposes, the test plan should be the same as the one used for the initial testing.
Number of samples/products
The appropriate number of specimens depends on the applicable standard, test objective, product variability, destructive evaluations, comparison groups, and the level of confidence required. Although some methods can technically be performed using a single specimen, multiple specimens may be required or recommended to produce representative and defensible results.
Sample size
Specify the shape and dimensions of the samples to be tested.
Duration of the predictable real-life exposure
The expected service exposure informs how long the laboratory test should run.
Optional sample preparation
Specify if required: (a) cleaning, (b) scribing (ASTM D1654 or other), (c) edge protection if exposed.
Orientation (if required)
Specimen orientation should follow the applicable test method or specification. For ASTM B117 salt spray testing, specimens are typically positioned at an angle of 15° to 30° from vertical. However, certain industry-specific specifications, particularly in the aerospace sector, may require a different orientation, such as 6° from vertical. The applicable test requirements should be confirmed before testing.
Visual inspection
If specified, include the time interval at which mid-test visual inspections will be performed.
Post-test evaluations
Define which evaluations will be run after exposure and what acceptance criteria apply. These should be defined before testing begins.
“We see too many projects where the test method was chosen too late in the development process.”
— Michel Comtois, President, Micom Laboratories
SUMMARY
Key Takeaways and Next Steps
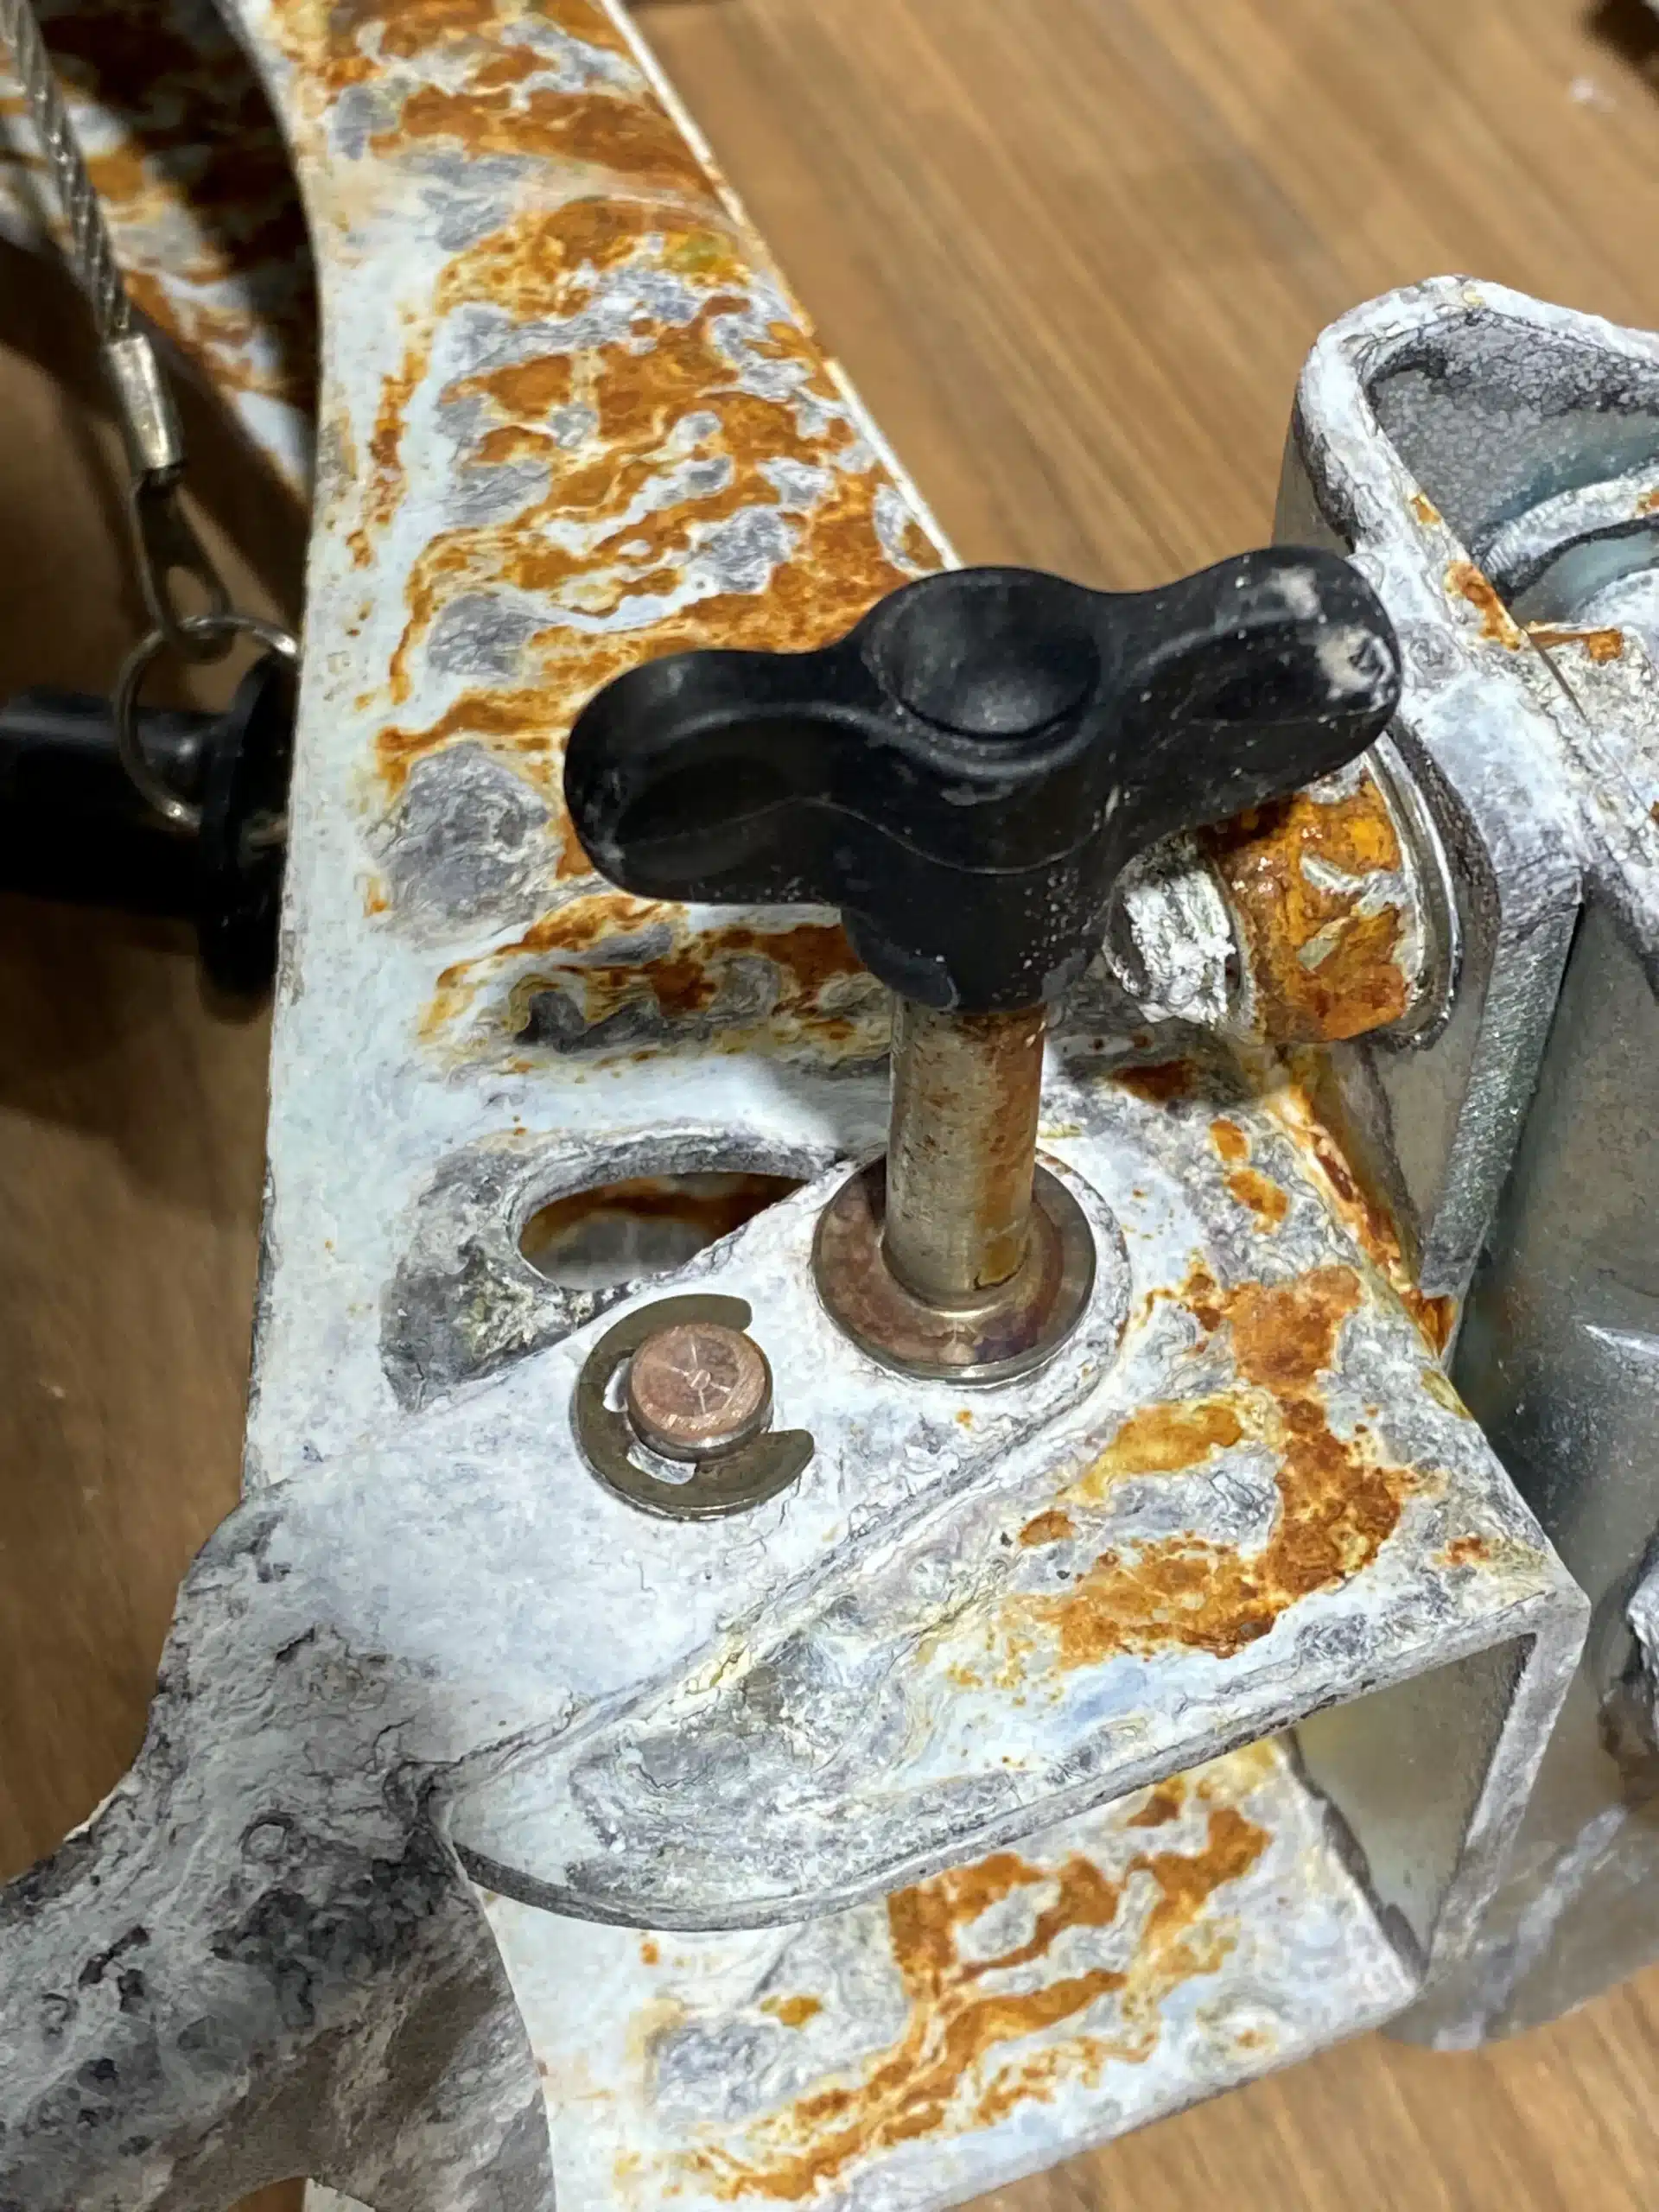 Corrosion is not a single phenomenon. It is a family of electrochemical processes that depend on the material, the environment, and the way a product is designed, assembled, and used. This is why corrosion performance cannot be reduced to a single number or a universal test duration.
A practical way to use this guide is to connect three elements early in a project: the expected service environment, the corrosion mechanisms most likely to occur, and the most appropriate test approach. When these are aligned, corrosion testing becomes a decision tool rather than a box to check. It helps you compare material options, qualify coatings and surface treatments, validate design decisions, and investigate failures when real-world results do not match expectations.
Salt spray testing remains a common starting point because it is repeatable, widely recognized, and cost-effective for comparative work and quality control. However, static salt fog conditions do not always reflect service conditions. When field performance matters, cyclic and combined tests can provide more representative results by introducing wet-dry cycling, humidity, temperature variation, and in some cases UV exposure. Selecting the right method is less about choosing the “most severe” test and more about choosing the test that best represents the environment and degradation modes your product will face.
When planning corrosion testing, it is also important to define evaluation criteria upfront. Mid-test observations and post-test assessments, such as rust rating, blistering, scribe creep, adhesion, and mass loss, can provide meaningful insights into degradation behaviour and can prevent unnecessary testing time. The best results come from a test plan that specifies the environment, duration rationale, sample preparation, orientation, inspection intervals, and acceptance criteria before the first sample is placed in a chamber.
If you are unsure which method or duration is appropriate, Micom Laboratories can help translate service conditions into a defensible test plan. A short scoping discussion can often clarify which standards are most applicable, whether a standard cycle needs adjustment, which evaluations will be most meaningful, and how many samples are required to support your decision.
Ultimately, the goal of corrosion testing is not only to “pass” a test. It is to understand risk, improve product durability, and avoid costly surprises in the field through informed material selection, design, and verification.
If you would like guidance on selecting the right corrosion test method, defining acceptance criteria, or building a test plan that reflects your real service environment, contact our material testing laboratory to speak with a material testing specialist.
- Fowler, S. (n.d.). Laboratory corrosion testing: 100 years of progress – realism and reproducibility with modern methods. Q-Lab Corporation.
- ASTM International. 2005. Corrosion Tests and Standards: Application and Interpretation. Page 23. Second Edition. ISBN 0-8031-2098-2.